At 2 pm on a Thursday in late October 2022, I approved a purchase order for 30 feet of ANSI 60 roller chain that was not the Tsubaki part listed in the engineering BOM. It was about 30% cheaper than the quoted original, so the projected savings on that one order were roughly $340. I signed it anyway.
The maintenance lead told me not to substitute. I wish I could say I had a technical argument. I had a spreadsheet argument.
The chain lasted about two months on a loaded index conveyor. It jumped a sprocket, scored the rail, and broke a guide bracket. The repair cost—new sprockets, labor, two shifts of downtime, plus the conversation with a customer about a late machine—was somewhere around $3,400. Don’t hold me to the exact split; we reclassified some costs. It was more than five times the savings I thought I had created.
I manage purchasing at a 90-person automation equipment company. For six years I have tracked the power-transmission side of the budget: roller chain, sprockets, bearings, linear guides, actuators, and the electric controls that make them move. Our yearly spend in that category is roughly $180,000. That is not infinite, but it is enough to make a $3,400 mistake visible.
I don’t have hard data on how often substitute components cause premature failures across the whole industry. I wish I had tracked every maintenance root cause that carefully from the start. What I can tell you anecdotally is that our most expensive unplanned repairs rarely came from a part that wore out too early. They came from my assumption that a part was interchangeable when it wasn’t.
The surface problem: I was looking at the price, not the system
When I cost-reduced that chain, I was doing my job as I understood it. Unit-price savings appear in procurement reports. The cost of a machine stop does not appear on the same line.
It is easy to blame a “bad part” after a failure. The deeper issue was that I had bought an engineering component as if it were a commodity. I was comparing the wrong specification.
The part-number trap
When the drawing specified a Tsubaki roller chain, I read the brand name as a preference. It wasn’t. It was shorthand for a list of decisions that the BOM does not spell out: which chain series, what allowable load at our drive speed, what lubrication requirement, what wear life assumption.
An ANSI 60 chain number standardizes some dimensions. It does not make every chain with that number identical. If you compare only pitch, width, and roller diameter, you are missing the material grade, link-plate geometry, and manufacturing tolerance that affect how the chain wears on a specific sprocket.
To be fair, the cheaper chain might have been perfectly good in another application. A substitute is not automatically dangerous. But “might be good somewhere else” is not an engineering decision.
The first hidden cost: chain wear was invisible
What did we do before that failure? We looked at the chain and listened. Noise and sag appeared when it was already late. By then, the sprocket teeth were changing shape. We weren’t replacing just a chain; we were replacing a chain plus sprockets and rail.
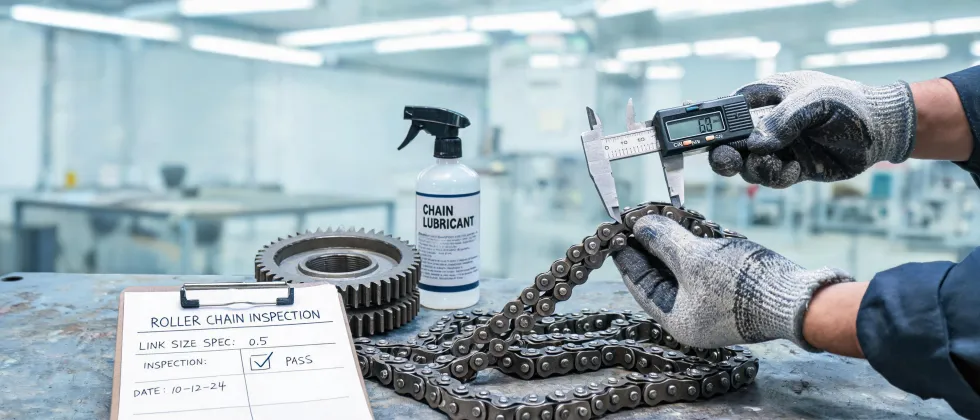
I have read enough maintenance guides since then to know that the measurement is not complicated. You measure chain elongation over a fixed number of pitches and replace it before it reaches the limit that makes skipping likely. In our PM routine, we use 2% as the trigger. Some equipment manuals specify a different number, so verify yours.
The chain wear indicator changed the routine
The Tsubaki chain wear indicator is a simple gauge. It made the biggest difference because it made measurement repeatable. It hangs near the lube cart. At each PM, someone takes five minutes to measure the high-cycle drives and records the number. If the number says 1.8%, we order the replacement chain. We replace it when convenient, not after an emergency.
As of our 2024 maintenance audit, that is still the routine. I don’t know the current tool part number by heart. The tool is not the expensive part. The discipline is.
The same pattern in linear guide carriages and electric actuators
I used to think the chain was a special case. Then I moved the same logic to linear motion components.
Linear guide carriages
Linear guide carriages look like commodity blocks. You can almost see why someone would order “same rail width, same length” and call it done. But a linear guide carriage is specified by more than width. There are accuracy classes, preload classes, and matching requirements with the rail. Two carriages can fit on the same rail and behave differently under load—one may be smooth, another may bind after a short period.
That does not mean a different manufacturer’s carriage will always cause trouble. But if the original assembly relies on low preload or high accuracy grade, and the replacement doesn’t state those values, the cheapest quote is also the riskiest quote.
Electric actuator controllers and stepper motors
Electric actuators are another version of the same thing. A reputable actuator vendor will tell you whether a product is mechanism-only or includes the motor. An electric actuator controller is not an accessory; it is the part that interprets the travel profile, current limit, and feedback.
The visible spec on an actuator may be stroke and force. The invisible spec is what happens at the end of stroke, how the motor current is managed, and how many cycles the mechanism can run before thermal trip. If you treat the actuator as a self-contained part and ignore the controller, you are buying half a system.
A few months ago, someone asked me, “How fast can a stepper motor turn?” I answered too quickly. The direct answer is “it depends.” Stepper motors lose torque as speed increases. A motor that spins 3,000 rpm with no load may not reach 400 rpm under the torque the machine actually needs, especially if the controller voltage is low. The torque-speed curve matters more than the max RPM.
The question underneath all of these
After six years of order records, I notice a pattern. Our expensive failures were not caused by exceptionally bad components. They were caused by not checking the system the component was part of. A chain lives with sprockets and lubrication. A linear guide carriage lives with a rail, preload, and axis load. An actuator lives with its controller and motion profile.
The hidden cost appears when the part number does not fully describe the job. That is why I now search for the original specification before I search for a lower price.
What I do now: a short checklist
I still buy on price. I don’t think that changes in procurement. What changes is when I allow price to be decisive.
- When the drawing lists a Tsubaki roller chain, I start with the full manufacturer part number and the original selection data. If a substitute is proposed, the engineer approves it with a documented comparison.
- We measure chain wear at scheduled PM intervals and use the Tsubaki chain wear indicator. If a measurement approaches 2%, it triggers a planned replacement instead of an emergency repair.
- For linear guide carriages, I ask for the complete code and confirm that it matches the rail, accuracy grade, and preload requirement.
- For electric actuators, I compare the mechanism, motor, controller, and cables as one system. If only one part is replaced, I ask the supplier what else will become incompatible.
- For stepper-driven axes, I ask for the torque-speed curve before saying yes to a motor or driver. The label speed is not enough.
The goal is not to avoid substitutes or to buy the most expensive brand. The goal is to make the total cost visible. An informed customer asks better questions. In my case, asking those questions earlier would have saved more than a spreadsheet line.