The line went down at 2:40 on a Tuesday. Not a dramatic crash, just the sound of a gear drive getting louder, with a little metallic click at the end of each revolution. I knew that noise. I also knew the next hour would involve a decision I wasn't ready to make: repair the old gearbox, replace it with a modern gear drive, or find a part that might not exist anywhere except in someone's dusty stockroom.
Full disclosure: I'm not the maintenance engineer. I'm the person who manages the maintenance budget. Over the last seven years at a 165-person packaging plant, I've approved about $1.8 million in MRO purchases. That sounds like a lot, but it includes every hydraulic hose, spare filter, and worn limit switch, not just capital parts. I've also learned to see the difference between the low quote and the actual cost.
The failing unit was what the maintenance paperwork called a gear drive. It had been on that case packer since the machine was installed, and nobody had ever replaced it. The nameplate was worn enough to make searching painful. The first distributor said no cross reference. The second one said call back next week. That was when I ended up in the same rabbit hole that probably brought you here: what happened to pete jackson gear drives?
To be clear, our failing component was not a Pete Jackson gear drive. It was just old and orphaned, no better for being original. When I searched the name, I found forum threads and old listings, not a reliable source of new units. What happened to pete jackson gear drives? Honestly, I'm not sure. My best guess is that the product line faded from mainstream distribution as applications moved on. But what mattered from my desk was simpler: the product was no longer easy to buy, and a maintenance plan built around a difficult-to-buy part isn't really a plan.
So I slowed down. Instead of ordering parts in a panic, I walked to the line with the maintenance lead, and we did the check that should have happened months earlier. Measure, photograph, look up part numbers, repeat. The gear drive had failed, but the conveyor chain wasn't far behind. That second discovery changed the project from a patch to a proper repair.
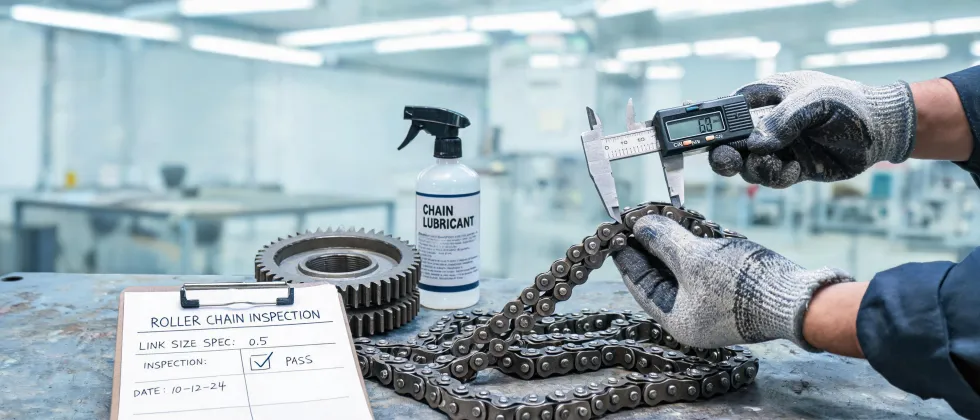
The chain turned out to be a Tsubaki conveyor chain that had been working for years. Honestly, it looked fine at a glance, which is why it bothered me. When we measured pin wear across the working section, a 3-foot span was 2.8% longer than the catalog limit. I didn't want to shut the line down a second time, so the chain replacement became part of the same project.
Here's where the Tsubaki roller chain catalog earned its keep. I know catalogs don't sound exciting. But when you're buying a replacement chain, the part number alone is not enough. You have to match pitch, roller diameter, attachment spacing, and working load. The catalog table made me confirm the chain we needed, not just the chain that a reseller preferred to sell. It also helped us check the sprockets so we didn't change the shaft center distance by accident.
The 24V side quest
While the gearbox was still off-site, the plant engineer asked if we could also replace a troublesome air cylinder on the same line. The cylinder indexed cartons into a lane, but the air supply was wet enough to cause repeated regulator failures. He wanted an electric operator so the speed and damping could be set without relying on compressed air.
I asked one vendor for a linear actuator 24v. The obvious candidate was a lead screw linear actuator, because the stroke length and cycle rate were within its rated capacity. The actuator itself cost more than a new pneumatic cylinder. But before I ruled it out, I calculated the total 36-month cost: electricity for the compressor, repair hours, downtime from moisture, and the cost of keeping an undersized dryer working.
The electric option was about $870 more upfront and roughly $1,100 cheaper over three years once compressed-air losses were included. We installed the lead screw linear actuator. It is not the fastest unit on the line, but it doesn't care if the air dryer has a bad day.
The part-number trap
The mistake I keep trying to avoid is buying by part number alone. A part number is an address, not a specification. It doesn't tell you whether a component was designed for high temperature, high shock, or high duty cycle. The same nominal size can be made with different clearances and materials. That's why I'm careful with the word equivalent.
Two years before this outage, I approved a lower-cost replacement chain because the seller called it equivalent to the original Tsubaki chain. It cost $220 less. It lasted about eleven months before it stretched enough to stop a photo eye and trip the line. The total cost of that short cut was about $4,800 in labor, lost product, and urgent freight. So I became the annoying person who asks for a catalog page before signing a PO.
What the repair finally taught me
In the end, we swapped the orphaned gear drive for a current-model unit with the same frame size. The chain is a Tsubaki conveyor chain, and the part number is written in permanent marker on the maintenance cabinet. The air cylinder is gone, replaced by a lead screw linear actuator. None of those were the cheapest individual choices. The whole project was around $14,000. That hurt. But the line has now run for nine months without a repeat failure, and the next inspection is already written into the schedule.
I still don't have a neat answer for what happened to pete jackson gear drives. I don't think I need one. The lesson from this repair isn't about one product line. It's about paying attention before the sound changes and buying parts that still have a future. Five minutes with a wear gauge and a current catalog is cheaper than another emergency Tuesday.