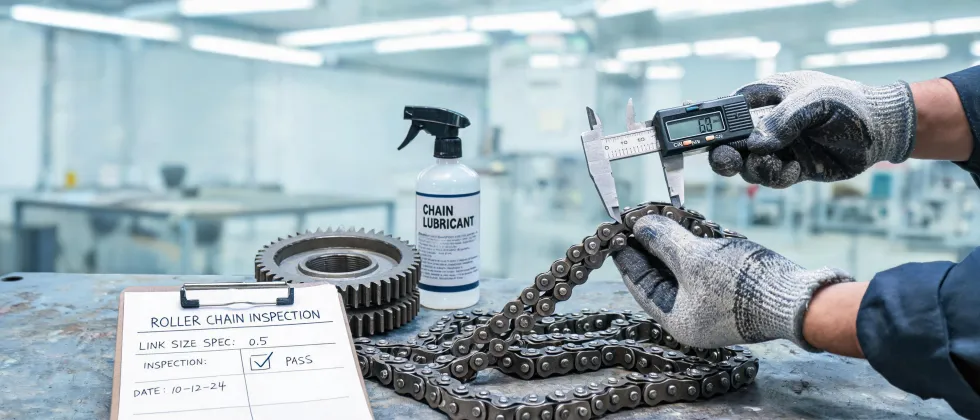
I manage procurement for a 200-person packaging plant. For the last six years, I have tracked every maintenance invoice in our cost system. Last year alone, those invoices totaled about $180,000. One pattern keeps showing up: we buy replacement parts based on the ticket price, not the total cost. This article compares two ways to handle a failing motion drive—keep replacing the timing belt, or switch to a Tsubaki chain setup—and how a Tsubaki chain wear indicator changed the way I look at maintenance.
If you are searching for a 'Plano timing belt replacement,' this comparison should matter to you. The question is not whether a belt can work. The question is how often you will pay to make it work again.
The comparison framework I used
I compared the belt route and the chain route on three things:
- Total cost over 36 months, including labor and downtime
- How much warning you get before failure
- What speed actually looks like under load
This is the framework I wish we had used in 2022. In March 2023, our carton conveyor stopped three times in one month. The first stop was a stretched timing belt. The second was a cracked belt. The third was a tensioner damaged by the first two failures.
I pulled the purchase history. We had replaced that belt four times in 14 months. Each replacement cost about $380 in parts and two hours of line downtime. Our maintenance lead suggested a Tsubaki chain conversion: $640 for chain and sprockets, plus a half-day installation. I resisted (which, honestly, was partly because I didn't want to justify the budget). The belt fix was a small PO. The chain conversion was a bigger expense and a new alignment step.
When I compared the belt receipts and the chain quote side by side, I finally understood why the expensive part was cheaper. The belt had no wear signal. It failed. We replaced it. The countdown restarted. The chain had a measurement we could track.
Dimension 1: Total cost is not the ticket price
Let's use our numbers. Four belt replacements in 14 months at $380 each, plus two hours of line downtime per event. At our internal rate of $200 per hour for downtime, the fully loaded replacement was about $780. Four events came to about $3,120 in 14 months.
The chain route cost $640 in materials and $400 in installation. Twenty-four months later, the chain still had measurable life left. The belt route would have needed about six more replacements in that same window. Over 36 months, the belt plan costs roughly $8,000. The chain plan costs about $1,040. That is not a small difference.
I verified the part numbers in the official tsubaki-chain catalog (accessed January 2025), not a reseller's shortcut listing. Searching 'chain tsubaki' can bring up aftermarket parts that look identical in photos. They may even fit. But the wear rate is not in the listing.
There is also the hidden cost of the conversation. After the second belt failure, maintenance asked for a root-cause meeting. The meeting took an hour. It didn't fix anything. It just confirmed that nobody wanted to approve another belt. You can't put that on a quote, but it is part of the total cost.
Dimension 2: The Tsubaki chain wear indicator makes the invisible visible
The timing belt gave us no warning. It looked fine until it didn't. Chain is different. A Tsubaki chain wear indicator measures elongation in the pins and bushings. Once we bought one, we checked every quarter. The indicator replaced a guessing game with a maintenance schedule.
Let's be honest about the indicator. It is a physical gauge, not a magic sensor. You still have to train someone to use it, and you still need a habit. The advantage is that the data is repeatable. Two different mechanics can measure the same chain and get the same number. You can't do that with a timing belt's 'looks okay' check.
For the record, the chain pitch we used was standard ANSI B29.1 80 series. That makes sourcing easy. It also makes it easy to buy the wrong thing if you don't verify the Tsubaki part number.
Dimension 3: Speed only matters if it holds up
Nobody asks what a component can do at idle. They ask what it can do under load. I hear the same thing when engineers ask 'how fast can a linear actuator move.' The no-load speed of a reciprocating linear actuator can look impressive. Under a real payload and a three-shift duty cycle, the effective speed is different.
We tested a reciprocating linear actuator on an indexing station in Q4 2024. The spec showed 20 inches per second. At 60 percent duty cycle with an 18 pound load, the actual cycle speed was 11 inches per second. We bought based on the tested number, not the marketing number.
The same logic applies to the belt versus chain decision. A timing belt can have a high theoretical speed limit. If it loses tension under heat or shock load, your effective throughput is whatever the downtime allows.
Speed also affects actuator selection. If you oversize for speed, you may pay a premium for the motor and controller. If you undersize, you get nuisance trips. The useful question is 'how fast can a linear actuator move this specific load, this many times per hour, for this many months?' Not just 'how fast can a linear actuator move.'
What a 'Plano timing belt replacement' quote really includes
Let's be fair to the belt. A single Plano timing belt replacement is not a bad job. If a machine has run on a belt for ten years and you just want it back to spec, replace the belt. The trap is treating that replacement as a permanent fix.
I have seen replacement quotes from $250 to $600 for the same job. The low quote did not include a new tensioner. The higher quote included a damper. Neither included the cost of the next failure. Maybe you are not in Plano. The point holds anywhere a belt replacement has become a repeating event.
What I would choose now
If the drive is light, simple, and you can schedule downtime, a timing belt replacement is fine. The key is to budget for the next one.
If the drive is critical, shock-loaded, or washed down, install a Tsubaki chain and use the wear indicator. The upfront cost is higher, but the cost per hour of operation is lower.
For linear motion, do not start with 'how fast can a linear actuator move.' Start with the speed curve under your load and your duty cycle. A reciprocating linear actuator with an honest speed curve is a better buy than one with a single impressive number.
I went back and forth on the chain conversion for two weeks. The belt was easier to approve. The chain required more money upfront and the maintenance team had to learn one new alignment step. In the end, I chose the chain because I would rather pay for a part I can measure than rent a fix I cannot.
What you can measure, you can plan. What you can plan, you can budget.
Our procurement policy now requires a TCO line on every replacement over $500. That policy came directly from this comparison. It has already saved us from two other 'cheap' parts that would have failed the same way.