-
1. Load and speed: where each drive earns its keep
-
2. Maintenance and environment: the part nobody puts on the spec sheet
-
3. Ordering the right part: catalog, diagrams, and the five-minute rule
-
4. Timing belt warning signs—and the chain equivalents
- 5. Sometimes the decision isn’t belt vs chain at all
-
6. So what do I order?
I’m the office administrator for a 220-person packaging operation. That means I buy replacement parts nobody thinks about—until one of them stops a line. When maintenance calls and says a machine is down, they don’t want a lecture; they want to know where the part is and how fast it will get here.
I’ve ordered a lot of Tsubaki chain over the years, and more timing belts than I expected when I took over purchasing in 2020. One question keeps coming back from people outside maintenance: why not use a chain instead of a timing belt? The two can look similar if you squint, and both transmit rotary motion, but they are designed for different realities. This is the comparison I run through when I have to choose.
A timing belt is not just a quieter chain, and a roller chain is not just a heavier belt. Both move power, but they get ordered differently, maintained differently, and fail differently.
1. Load and speed: where each drive earns its keep
Roller chain is steel pins, bushings, rollers, and side plates. That construction handles shock, vibration, and occasional abuse much better than a rubber belt can. Slow, heavy, and dirty? That is chain territory. Our pallet conveyor starts and stops under load all day; a belt drive would have a short life there.
A timing belt is a different animal. It’s also called a synchronous belt because its teeth lock into pulley grooves, so it doesn’t slip under normal operation. It runs quieter than a chain, picks up no lubrication mess, and handles higher speeds with less vibration. The tradeoff is load capacity: a timing belt can move light-to-moderate loads very precisely, but it is not my first choice for shock loads or heavy starting torque.
The conclusion I keep landing on: if the drive runs slowly and carries heavy or jerky loads, choose a roller chain. If the drive runs fast and clean and needs synchronized motion, choose a timing belt. They stop being “the same job” once you know what the machine actually does.
2. Maintenance and environment: the part nobody puts on the spec sheet
Chain drives need lubrication. If you skip it, the pins wear, the chain stretches, and the sprockets wear faster. We ran one conveyor with a dry chain for a while back in 2021—it got noisy, then stiff, then unreliable. The fix was regular dry-film lube, but it had to become a habit. Chain is tough, but it is not self-maintaining.
Timing belts are easier in that regard, and I have mixed feelings about them because of it. On one hand, no lube means less mess and fewer contamination worries, which matters on a packaging line. On the other, belts are less forgiving of misalignment and tension errors. A misaligned belt wears on the edges. An over-tensioned belt taxes bearings and builds heat. Oil or solvent can ruin the rubber. The belt itself doesn’t need grease, but the drive still needs attention.
My practical rule: where grease is unwelcome and loads are moderate, a timing belt usually wins. Where loads are heavy or the environment is harsh, chain wins. (Unfortunately, nothing in a plant runs itself.)
3. Ordering the right part: catalog, diagrams, and the five-minute rule
This is the dimension I care about most because I’m the one who feels the mistake. A wrong replacement part is downtime multiplied by shipping time.
Roller chain is reasonably straightforward. The chain number is usually printed on the side plates—an RS80 or similar—and sprockets are standardized. Even so, I open the Tsubaki chain catalog before placing the order. The catalog lists pitch, roller dimensions, tensile strength, and cross-references with sprockets. It takes two minutes and has saved me from more than one embarrassing “wrong size” phone call.
Timing belts are less forgiving to order. The spec is sometimes printed on the back of the belt, but it can be faded, dirty, or partially worn off. If the old belt is off the machine, I ask the maintenance team for three numbers: tooth pitch (the distance between teeth), belt width, and tooth count. Belt length is pitch times the number of teeth. The pulley groove profile also has to match; an 8 mm pitch belt and a 14 mm pitch belt are not close enough to “make work.”
If the part number is readable, most of that is encoded in it. If it isn’t, or if the machine has been modified, I ask for the routing drawing from the manual—the timing belt diagram. A diagram removes the guesswork about how the belt routes and whether what’s on the machine is the original configuration. That is the difference between ordering with confidence and gambling with a lead time.
The rule I repeat to our staff: five minutes of verification before the order beats five days of waiting after the wrong order. It sounds like a slogan, but it is the most expensive lesson I learned in this job.
4. Timing belt warning signs—and the chain equivalents
I became interested in warning signs in 2024, when a labeler lost registration. We checked sensors first, recalibrated a few times, and finally found that worn belt teeth were allowing the belt to jump one tooth under startup load. The belt cost about $40. The troubleshooting cost hours of production time.
If you maintain equipment with timing belts, these signs should trigger a replacement, not another month of “watch it”:
- Cracks in the belt back or at the base of the teeth, especially across more than a few teeth
- Frayed edges or exposed reinforcing cords
- Shiny, glazed areas or rubber that feels hard and brittle
- Squealing or chirping when the drive starts or stops
- Unexplained position drift, registration errors, or a suspected tooth skip
For roller chain, the list looks different, but the principle is the same:
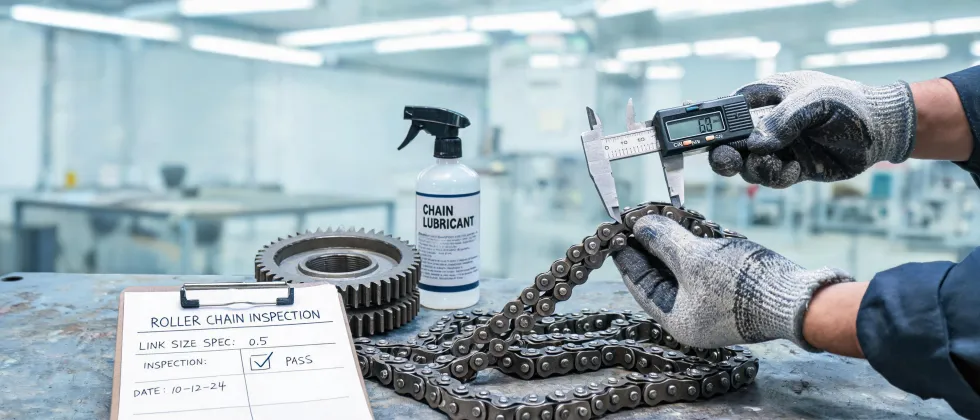
- Stiff or kinked links; a chain that doesn’t lie flat when laid on a bench
- Visible rust or pitting on pins and side plates
- Chain slack that keeps growing, or chain that rides high on the sprocket teeth
- Noisy slapping against a guide or guard during normal running
On elongation, don’t hold me to an exact percentage for every chain series—the maintenance team uses a wear gauge—but somewhere between 2% and 3% stretch is the general area where roller chain starts causing problems with sprocket fit.
Preventive replacement is a planned twenty-minute job. Emergency replacement happens at 4:47 on a Friday. I’d rather explain a preventive part order to finance than explain another line shutdown.
5. Sometimes the decision isn’t belt vs chain at all
For vertical moves, a standard drive comparison can lead you astray. If the task is to lift a load vertically in a compact space, a chain column lifter may be the better answer. The Tsubaki ZIP Chain Lifter, for example, uses interlocking chain links that form a rigid column as it extends, so it can push loads upward without a long rod or scissor mechanism. It isn’t a replacement for a timing belt; it’s a different solution to a different motion problem.
What’s a stepper motor?
When a machine does precise indexing, I also ask what kind of motor is driving it. A stepper motor is a brushless motor that rotates in fixed increments, typically 1.8 degrees per step. Every electrical pulse moves the shaft by that fixed amount, which lets a controller position light loads without an encoder. For that reason, stepper motors show up in labelers, printers, and small indexing conveyors, and they are often paired with timing belts rather than roller chain. The belt is clean, quiet, and precise enough for those low-mass axes.
Including this matters because the chain-versus-belt question is usually hiding a bigger design question. If the right solution is an electric lifter for vertical motion or a stepper-driven belt for a light indexing axis, comparing roller chain and timing belt alone won’t get you there.
6. So what do I order?
If you push me for a practical answer, I choose by scenario:
- Heavy loads, shock starts, dirty surroundings, or low speeds: roller chain. Verify the chain number in the chain catalog.
- Light-to-moderate loads, higher speeds, clean environment, or no-lubrication zones: timing belt. Order with the part number and the diagram when available.
- Compact vertical lifting or replacement of a pneumatic cylinder: consider an electric chain lifter like the ZIP Chain Lifter.
- Precise low-load indexing: look at a stepper motor paired with a toothed belt.
I still have mixed feelings about both technologies. Chain is tough, but it asks for regular care. Timing belts fail less often in clean service, but their failures can be confusing, especially when a belt jumps teeth without any visible damage. So my advice as a buyer is not “chain forever” or “belt forever.” It’s to compare the actual load, environment, part identification path, and warning signs before you spend money on a replacement. The right answer is usually hiding in one of those four details.